Portable grinder wheel vs grinding train wheel: are they interchangeable?
Portable grinder wheel vs grinding train wheel: are they interchangeable?
No — not across the two classes. A portable machine wheel runs 125-150 mm in diameter on a spindle fixing — M20 thread, 5/8-inch arbor or a bolt-on pattern — at 6,000-7,500 rpm. A grinding train wheel runs 230-280 mm in diameter, 25-105 mm thick, on a 120-154 mm bore with hub or flange mounting, at 2,730-3,630 rpm. Both are rated 50 m/s, both are resin-bond with glass-fibre reinforcement and both are inspected wheel by wheel to the same standard — but the fixing, the guard envelope and the mass are different, so a wheel from one class does not mount on the other and must not be forced to. The place where the classes genuinely meet is the 150-180 mm switch-unit band, which is shared between portable machines and the light turnout units of production trains. That is a narrow overlap, not an exchange rate.
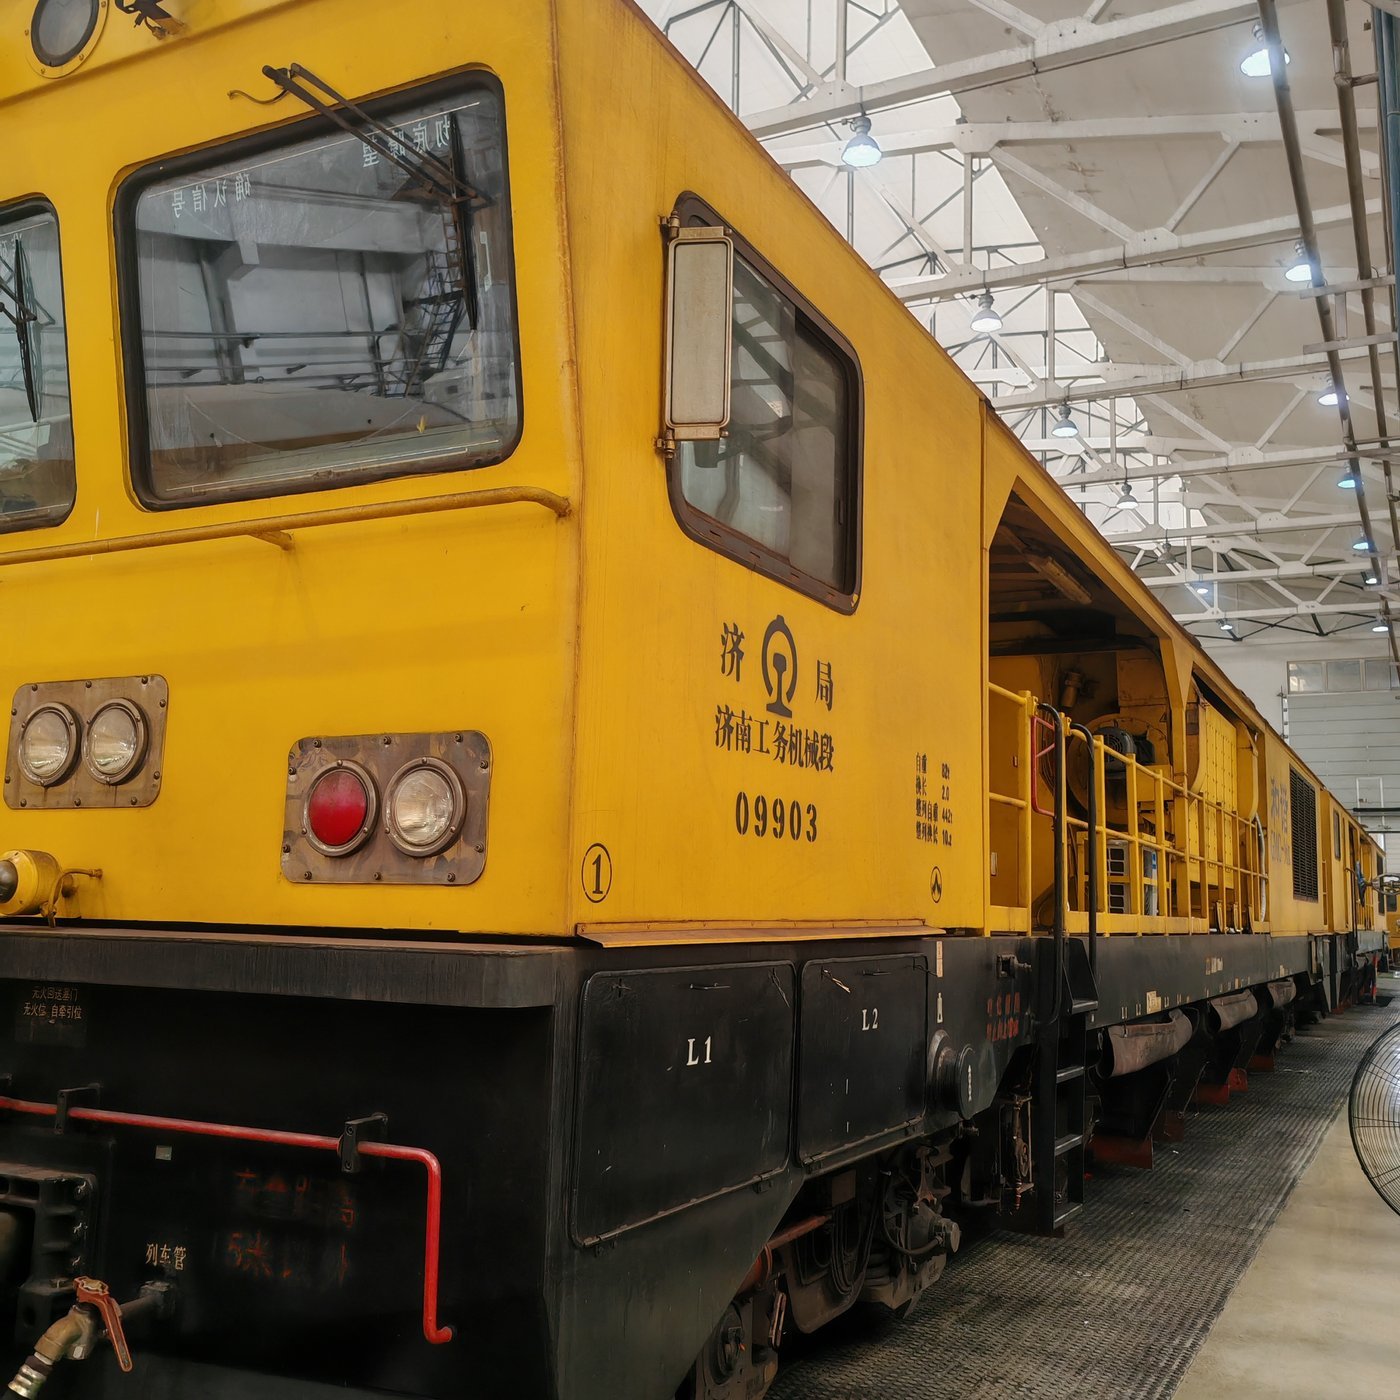
Two classes, side by side
| Attribute | Portable machine wheel | Grinding train wheel |
|---|---|---|
| Typical outside diameter | 125-150 mm | 230-280 mm |
| Typical thickness | 20-80 mm | 25-105 mm |
| Fixing | M20 spindle thread, 5/8-inch arbor, bolt-on or dual-step bore | 120-154 mm bore, hub or flange mounted |
| Rated spindle speed | 6,000-7,500 rpm | 2,730-3,630 rpm |
| Maximum working speed | 50 m/s marked on the wheel | 50 m/s marked on the wheel |
| Wheels per machine | One per head, hand or lever fed | Eight per grinding unit; 16 to 96 wheels per train |
| Feed and control | Operator controlled, spot and joint work | Power fed, programmed pass plan across kilometres |
| Balance regime | Static balance coefficient K=0.4 under Q/CR 1-2014 | Same coefficient, same standard |
| Inspection | Appearance, mated surfaces, dimensions, static balance, rotation strength — wheel by wheel, Q/CR 1-2014 §6.2.2 | Identical regime, no relaxation for volume |
Read the first and third rows together and the whole question resolves. The nominal diameter is what people compare; the fixing is what actually decides whether a wheel can be fitted at all.
Why the boundary is physical, not commercial
- The fixing does not convert. An M20 threaded spindle cannot hold a wheel built around a 154 mm bore, and a portable wheel has no hub face for a train head to clamp. There is no adapter that makes this legitimate — and an improvised one is a burst waiting to happen.
- The head is designed around a diameter band. A machine's guard and its speed control are set for the wheels it was built for. On a Geismar MC3 class turnout grinder, for example, the spindle runs at 3,600 rpm with wheels up to 254 mm and drops to 3,300 rpm at 260 mm — the machine itself changes speed when the wheel diameter changes, which is what keeps the rim speed inside the rating. That logic exists because the diameter band is part of the design. More on that machine in what the Geismar MC3 rail grinder is.
- The mass is an order of magnitude apart. A production train wheel in 260×90×154 mm weighs about 9 kg; a 250×75×150 mm wheel about 7.48 kg; a 180×105×90 mm switch-unit wheel about 6.2 kg. A hand-guided machine is not built to spin that mass, and a train head gain nothing from a wheel too light to be clamped by its hub.
- The same 50 m/s means very different rpm. Surface speed is what the rating describes, and it is set by diameter and speed together: n = 954,930 ÷ D gives the rpm for 50 m/s with the diameter D in millimetres. That single line explains why the two classes carry such different speed markings, and why a wheel's marking — not the machine's convenient speed — is the limit. The full arithmetic is in maximum operating speed for a rail grinding wheel.
- Getting it wrong has two failure modes. Overspeed — fitting a small wheel to a faster spindle than its marking allows — risks a burst. Undersize — fitting a smaller diameter than the head was designed for — exposes the spindle, changes the contact angle and reduces surface speed until the pass no longer cuts.
What the arithmetic looks like in practice
| Wheel diameter | rpm for 50 m/s | Class and typical marked speed |
|---|---|---|
| 125 mm | 7,639 rpm | Portable, marked 7,500 rpm |
| 150 mm | 6,366 rpm | Portable and light turnout, marked 6,000 rpm |
| 230 mm | 4,152 rpm | Light turnout units and custom sizes |
| 250 mm | 3,820 rpm | Production train, marked 3,280 rpm at 250×75×150 |
| 260 mm | 3,673 rpm | Production train, marked 3,630 rpm |
| 350 mm | 2,728 rpm | Production train, marked 2,730 rpm |
Every marked speed in that table sits at or just under the calculated value, which is how a catalogue should read. Now the consequence for substitution. A production wheel that has worn from 260 mm to 230 mm still turns at 3,630 rpm, but its surface speed has fallen from 49.4 m/s to 43.7 m/s — a drop of about 11.5%. In other words, a train wheel wears into a slower-cutting wheel, and a smaller wheel put on a train head does not cut faster — it cuts slower. That is the physical reason portable-class wheels are not used as an economy measure on production heads.
The one band where the classes genuinely meet
Between roughly 150 mm and 180 mm the same wheel can appear on a hand-guided machine and on a light turnout unit of a production train. What decides it is the bore and the mounting, never the diameter alone.
| Size | Fixing | Where it is used |
|---|---|---|
| 150×56×M20 weld-zone wheel | M20 spindle | Weld collar removal on Geismar and Robel 150 class machines — 150×56×M20 |
| 150×65×M20 | M20 spindle | Turnout and switch work on Geismar and Robel 150 class — 150×65×M20 |
| 150×70×55 bolt-mounted and dual-step bore formats | Bolt-on pattern | Same machine family where the fixing is bolted rather than threaded — bolt-mounted 150×70×55 |
| 150×75×32 mm | 32 mm bore | Geismar and Robel 150 series urban rail — 150×75×32 |
| 150×77×M20 and 150×80×5/8 inch | M20 and 5/8-inch arbor | Harsco RGH20C light turnout and urban rail units — 150×77×M20, 150×80×5/8 inch |
| 254×32×25.4 mm | 25.4 mm bore | Larger turnout wheels on Geismar and Robel machines — 254×32×25.4 |
| 180×105×90 mm | Switch-unit hub | Speno GMC16A switch units on production trains — 180×105×90 for GMC16A |
This band is why a well-run store keeps one 150-class line that serves both portable machines and light turnout units, instead of two. It is also why that same store keeps production wheels as a separate line matched to each grinding head — see 260×90×154 for PGM-48/96C, 250×75×150 for GMC96B and 260×83×154 for Loram C44/MFS.
Checking a substitution before you make it
- Bore and fixing first. If the bore and the mounting pattern do not match the spindle, stop. Everything after this is irrelevant.
- Diameter against the head's design band. Inside the band the machine's guard and speed control work as intended; outside it, neither does.
- Wheel marking against actual spindle speed. The marked maximum working speed governs. A machine is never allowed to exceed it, at any wheel diameter.
- Balance and condition. The unbalance allowance scales with wheel mass, so a balance figure from one size cannot be read across to another. Before fitting any wheel that has been stored, transported or dropped, carry out the checks in how to perform a ring test on a rail grinding wheel — with the caveat that a ring test screens for major cracks only and does not replace wheel-by-wheel inspection.
For the wider picture of what is and is not swappable between machines of the same class, see can one wheel fit different grinding machines, and for choosing between the two machine types in the first place, portable rail grinder vs full-size grinding train.
How the two classes are costed, and why they are not compared
The two wheel classes are consumed in different ways, so they are budgeted in different units.
- Train-class wheels are budgeted per pass-kilometre. One pass-kilometre is one kilometre ground once, so a campaign of 57.6 km ground three times is 172.8 pass-km. Wheel life is expressed the same way: on our heavy-haul programme at Shuohuang a wheel averaged 199 pass-km at 4.98 pass-km per millimetre of wear, and on the Hewu high-speed programme 214.22 pass-km at 4.28 pass-km per millimetre.
- Portable wheels are consumed by job. A 150-class wheel spends its life on weld collars, joint blending, turnout touches and spot defects, so its cost is driven by how many joints and defects you have, not by pass-kilometres.
Treating a portable wheel as a cheap train wheel therefore does not work on either basis: it cannot be fitted, and if it could, it would not deliver a production pass. If cost is the question, the lever is wheel life in pass-kilometres and removal per pass — see what actually drives the cost of a rail grinding wheel — not substituting across classes.
For machine-side background, see what a rail grinding vehicle is and the grinding vehicle range; for portable machine wheels, Geismar and Robel compatible wheels. Where a machine falls outside standard catalogue sizes, light customization solutions covers the custom bore and diameter route rather than a cross-class substitution.
Related questions you may also ask
Portable rail grinder vs full-size grinding train: which do I need? Can one rail grinding wheel fit different grinding machines? What is the maximum operating speed for a rail grinding wheel? What is a rail grinding vehicle? What is the Geismar MC3 rail grinder? More answers on rail grinder wheelsGet the right wheel for each of your machines
Send Molaton the machine model, the bore and mounting pattern, the spindle speed and the wheel size you run today. We will confirm the Molaton wheel for each machine separately — portable and production — and flag any size that needs a custom bore rather than a substitution.
Request a Wheel Matching Check
Are you looking for a reliable manufacturer of railway grinding and track maintenance equipment?
We can quickly provide customers with market analysis, technical support and customized services.
Safe Tracks Proven by China
- Name
- Phone
- *Title
- *Content