Rail Burning Prevention: Why Your Railway Grinder Wheel Choice Matters Most
Your tracks are our priority. Choose RailwayCare for reliable rail maintenance and superior rail grinding expertise.
Rail burning — the formation of a hard, brittle white etching layer (WEL) on the rail surface due to excessive grinding heat — is one of the most costly quality failures in rail grinding operations. A single burn incident can require re-grinding several meters of rail, or in severe cases, rail replacement. Understanding the root causes and selecting the right railway grinder wheel is the most effective strategy for eliminating burns entirely.
What Is Rail Burning and How Does It Damage the Track Structure?
Rail burning occurs when the temperature at the grinding interface exceeds the austenitizing temperature of rail steel — approximately 720°C for standard carbon-manganese rail grades. At this temperature, the surface layer transforms to austenite. When the passing railway grinder wheel moves on, the thin heated layer is rapidly quenched by the cold bulk metal beneath, forming martensite — a hard, brittle, and crack-sensitive microstructure.
- Appearance: Blue-black discoloration bands on the rail surface
- Hardness: 700–900 HV vs. 350–400 HV for normal rail
- Cracking risk: Martensite is brittle — thermal cracks initiate within hours of train traffic
- Fatigue life reduction: 50–70% reduction in rolling contact fatigue resistance
Five Root Causes of Rail Burning in Railway Grinder Wheel Operations
Burning is not a random event — it has five identifiable root causes, most of which are directly related to railway grinder wheel selection and operating parameters:
1. Wheel Hardness Too High
An excessively hard wheel bond holds dull grains too long, increasing friction force and heat generation before the grains finally fracture or release.
2. Grinding Pressure Too High
Excessive spindle pressure forces deeper grain penetration, generating more frictional energy than the rail can dissipate.
3. Speed Mismatch
Grinding too slowly increases contact time per unit length, concentrating heat input. Below 4 km/h, burn risk increases exponentially.
4. Insufficient Cooling
Low wheel porosity reduces air flow through the grinding interface. Heat accumulates rather than being carried away.
5. Poor Chip Clearance
Clogged wheel pores prevent grinding chips from evacuating, causing chips to be re-ground and generating additional frictional heat.
The Metallurgical Reality: What Happens Inside the Rail When a Railway Grinder Wheel Burns It
When a railway grinder wheel overheats the rail surface, a sequence of metallurgical transformations occurs within milliseconds:
- Temperature spike > 720°C: The surface layer transforms from pearlite to austenite.
- Heat conduction: The heat rapidly transfers into the bulk rail, creating a steep thermal gradient.
- Quenching: As the grinding wheel passes, the thin austenitized layer is quenched by the cold metal beneath at rates exceeding 100°C/second.
- Martensite formation: The rapid quench rate prevents the normal pearlite transformation. Instead, the surface becomes hard, brittle martensite.
- Crack initiation: The volumetric expansion associated with martensite formation creates high tensile residual stresses at the surface — cracks form within hours of train loading.
The damage is permanent. The only remedy is to grind away the entire martensitic layer, which may require removing 0.3–0.5 mm of rail material.
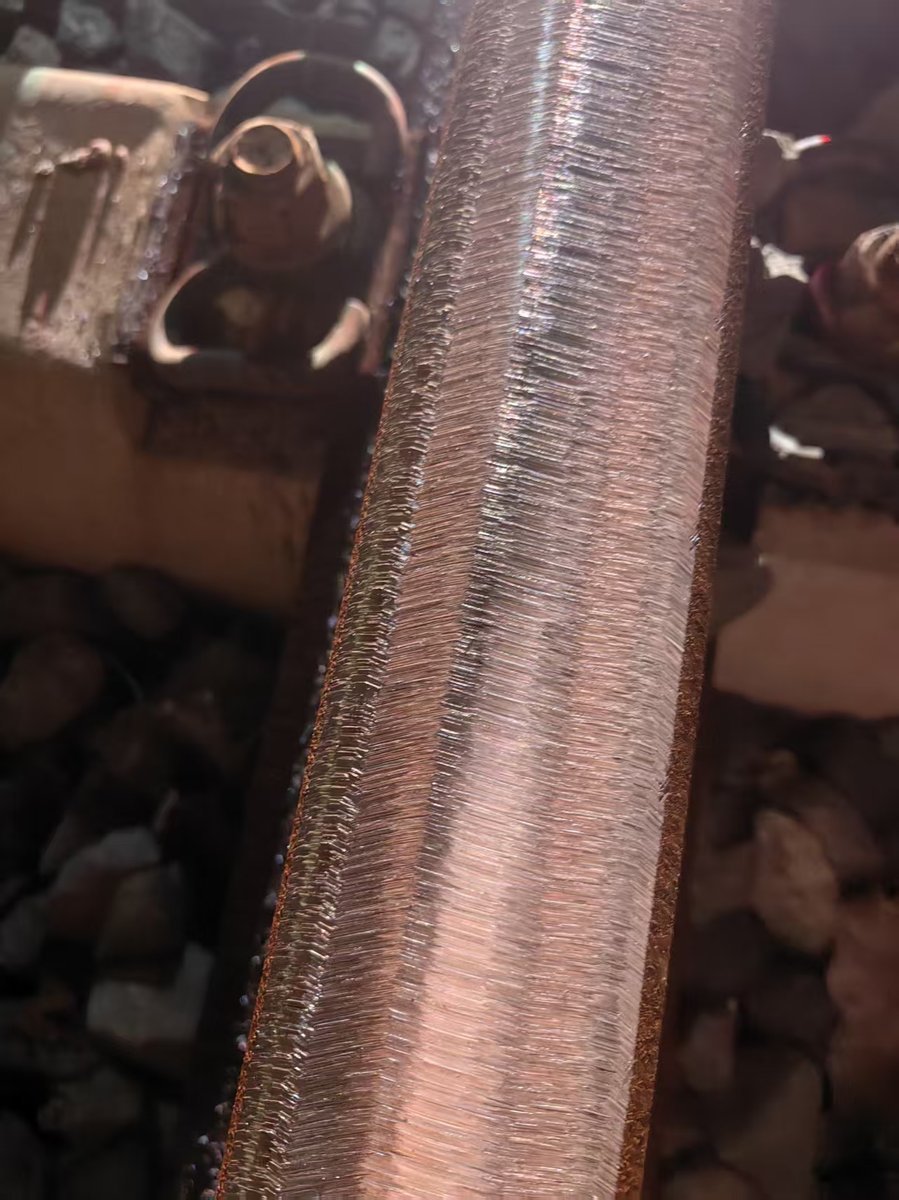
Preventing Rail Burns Through Proper Railway Grinder Wheel Selection
The most effective burn prevention strategy is selecting a railway grinder wheel that actively manages heat generation:
| Wheel Property | Burn Prevention Mechanism | Molaton Specification |
|---|---|---|
| Grain type | Self-sharpening grains reduce friction force | Zirconia alumina |
| Bond hardness | Optimized bond prevents grain glazing | Controlled hot-pressed |
| Porosity | Pores provide cooling air flow | 15–22% engineered porosity |
| Grain size | Smaller grains = finer chips = less heat | 24–36 grit range |
| Wheel density | Uniform density prevents hot spots | ±2% density variation |
Operating Parameters: The Speed-Pressure-Temperature Triangle
Even the best railway grinder wheel can produce burns if operating parameters are poorly selected. The relationship between speed, pressure, and temperature is non-linear:
- Speed (km/h) ↑ → Temperature ↓: Faster passes reduce contact time per unit area, lowering peak temperature.
- Pressure (MPa) ↑ → Temperature ↑↑: Temperature increases with the square of pressure — a 20% pressure increase can raise temperature by 40%.
- Density ↑ → Temperature ↑: Denser wheels have less porosity for cooling, increasing burn risk.
The safe operating window for each railway grinder wheel formulation is determined by testing. Molaton provides recommended operating parameter ranges with every wheel shipment.
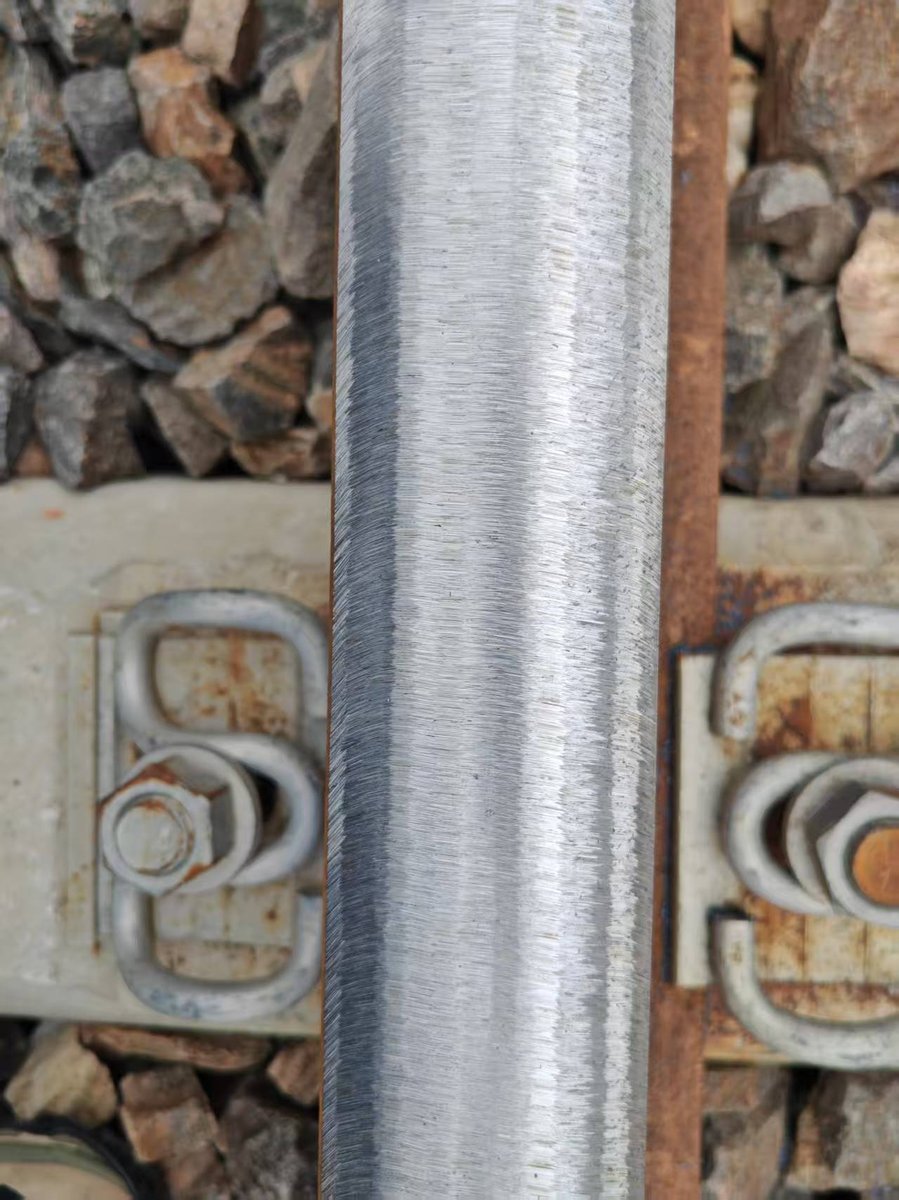
Molaton Zero-Burn Track Record: Harsco 96 Field Data
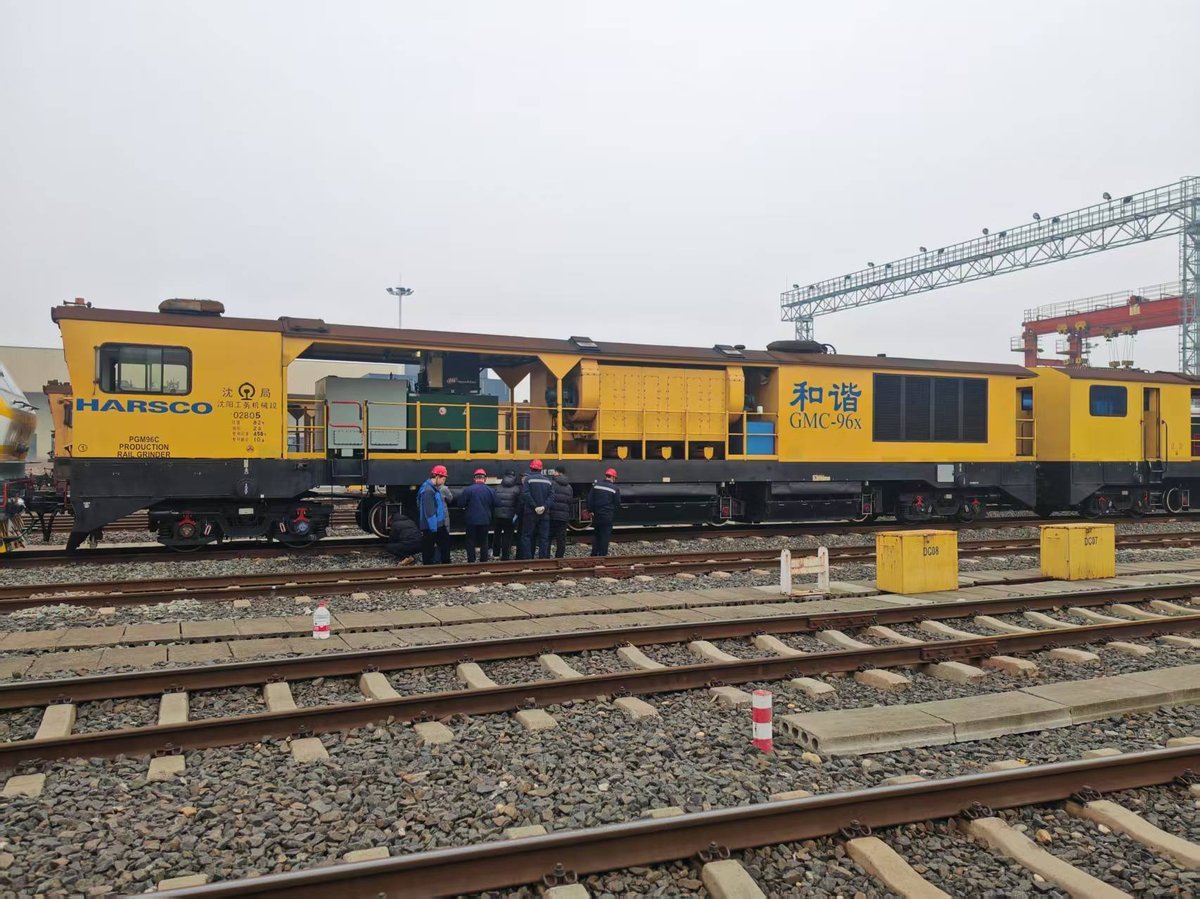
The most compelling evidence for effective burn prevention comes from field data. On a Harsco 96-head grinding vehicle operating on heavy-haul lines, Molaton hot-pressed zirconia alumina railway grinder wheel products achieved:
- Total grinding distance: 200+ km
- Burn incidents: Zero
- Average Ra: 6.2 μm
- Wheel life: 39.8 km average
- Grinding speed: 6–10 km/h
The combination of zirconia alumina grain self-sharpening, hot-pressed bond uniformity, and engineered porosity created a thermal management system that kept rail surface temperatures safely below the austenitizing threshold throughout the entire test campaign.
Burn Detection Methods and Acceptance Standards
Burns must be detected quickly during grinding operations to prevent rework costs. The accepted detection methods are:
Visual Inspection
Blue-black discoloration bands on the rail surface. The primary screening method but cannot detect sub-surface burns.
Magnetic Particle Testing
Reveals thermal cracks associated with martensite formation. Used for verification when visual indication is present.
Hardness Testing
Surface hardness > 450 HV indicates martensite. Portable Leeb testers are used for field verification.
Acid Etching
Nital etching reveals white etching layer. Definitive test but requires surface preparation.
The No-Blue-Band Rule: A Universal Grinding Quality Standard
Across the rail industry, a universal rule applies: the ground rail surface must show no continuous blue discoloration bands. This rule appears in every major railway's grinding specification, including:
- China Railway: High-speed rail grinding acceptance standard
- UIC 712: International rail grinding specification
- AREMA: American railway grinding standards
- Network Rail: UK rail grinding acceptance criteria
Achieving zero-blue-band compliance consistently requires a railway grinder wheel designed specifically for thermal management — which is exactly what Molaton's hot-pressed zirconia alumina product line delivers.
Comparing Burn Incidence: Hot-Pressed vs Cold-Pressed Railway Grinder Wheels
The manufacturing process directly affects burn risk:
| Parameter | Hot-Pressed (Molaton) | Cold-Pressed |
|---|---|---|
| Porosity control | ±1% target | ±3–5% target |
| Hardness uniformity | ±1 grade | ±2–3 grades |
| Burn incidence (field data) | <0.1% | 1–3% |
| Blue band occurrence | Rare, isolated | Occasional, systematic |
The superior thermal management of hot-pressed wheels reduces burn incidence by a factor of 10–30 compared to cold-pressed alternatives.
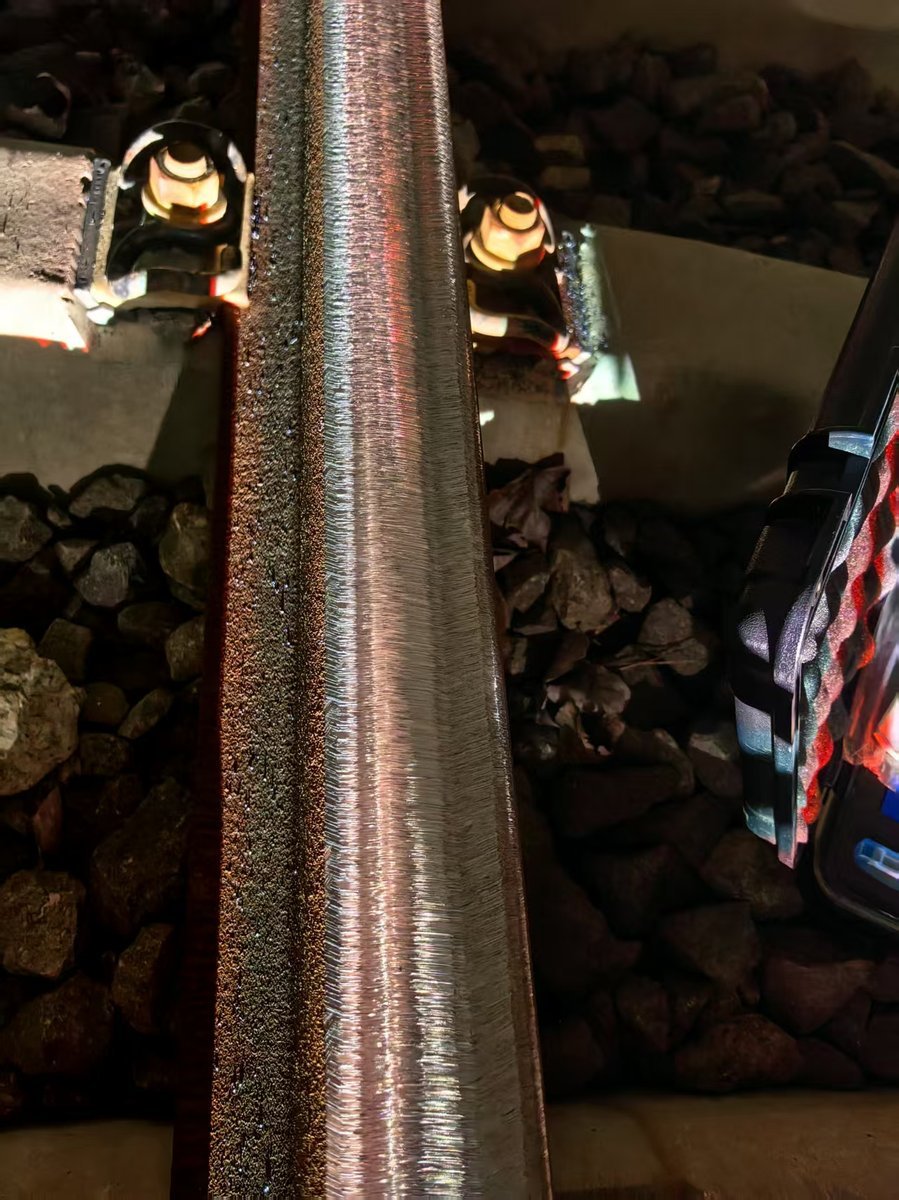
Selecting a Burn-Free Railway Grinder Wheel: Practical Recommendations
To eliminate rail burning from your grinding operations, follow these recommendations:
- Choose zirconia alumina grains: Their self-sharpening behavior produces the lowest friction heat of any abrasive grain suitable for rail steel.
- Specify hot-pressed bond: The uniform bond structure provides predictable wear and consistent thermal performance.
- Verify porosity >15%: Adequate porosity is essential for heat dissipation and chip clearance.
- Match wheel to machine: Different vehicles operate at different pressure and speed ranges — the wheel must be calibrated to the specific machine.
- Monitor grinding temperature: Use thermal crayons or infrared thermometers during qualification testing.
Molaton offers a dedicated burn-prevention railway grinder wheel series with enhanced thermal management features. Our engineering team can review your current operation and recommend the optimal specification to achieve zero-burn performance.
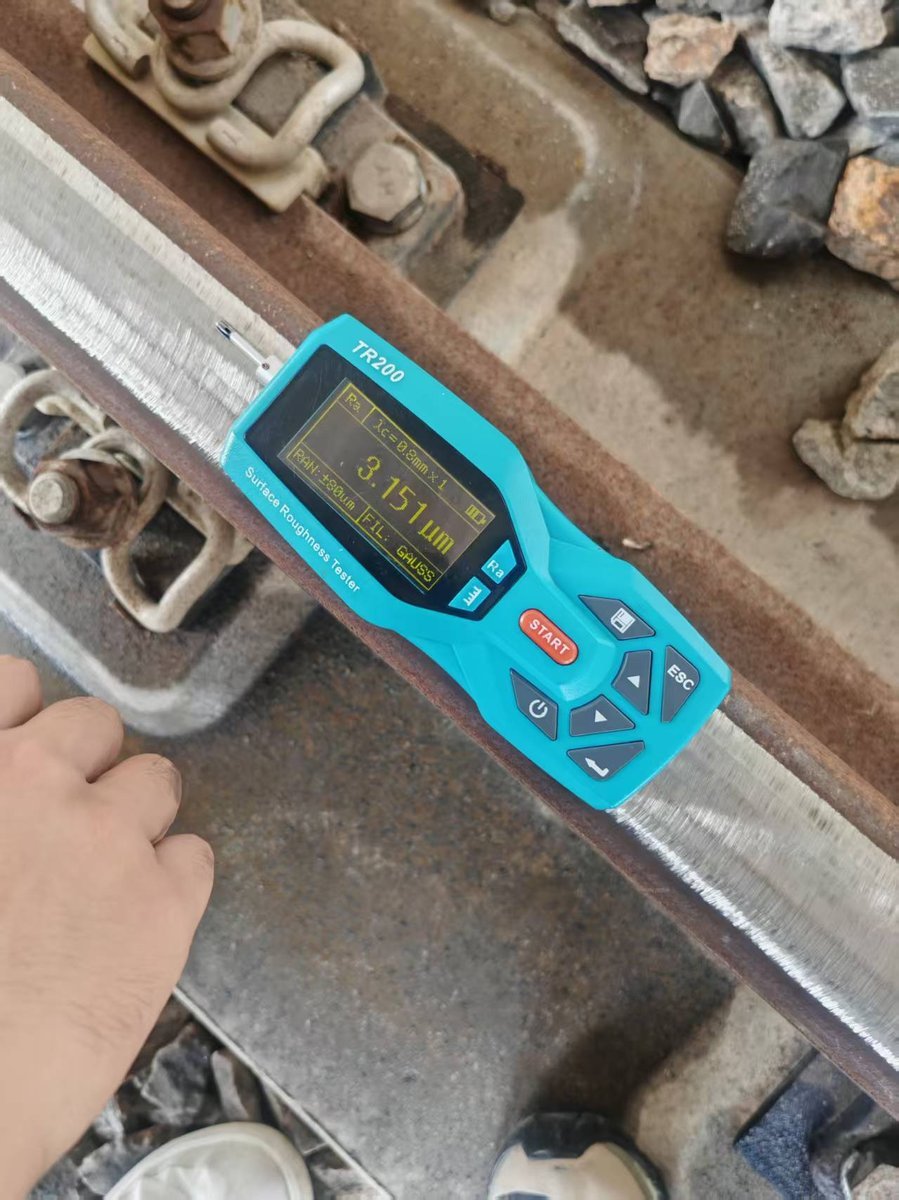
Additional Field Images: Molaton Railway Grinder Wheel in Action
Additional photographs from Molaton's railway grinder wheel field operations and manufacturing, providing more visual evidence of product quality and grinding performance.
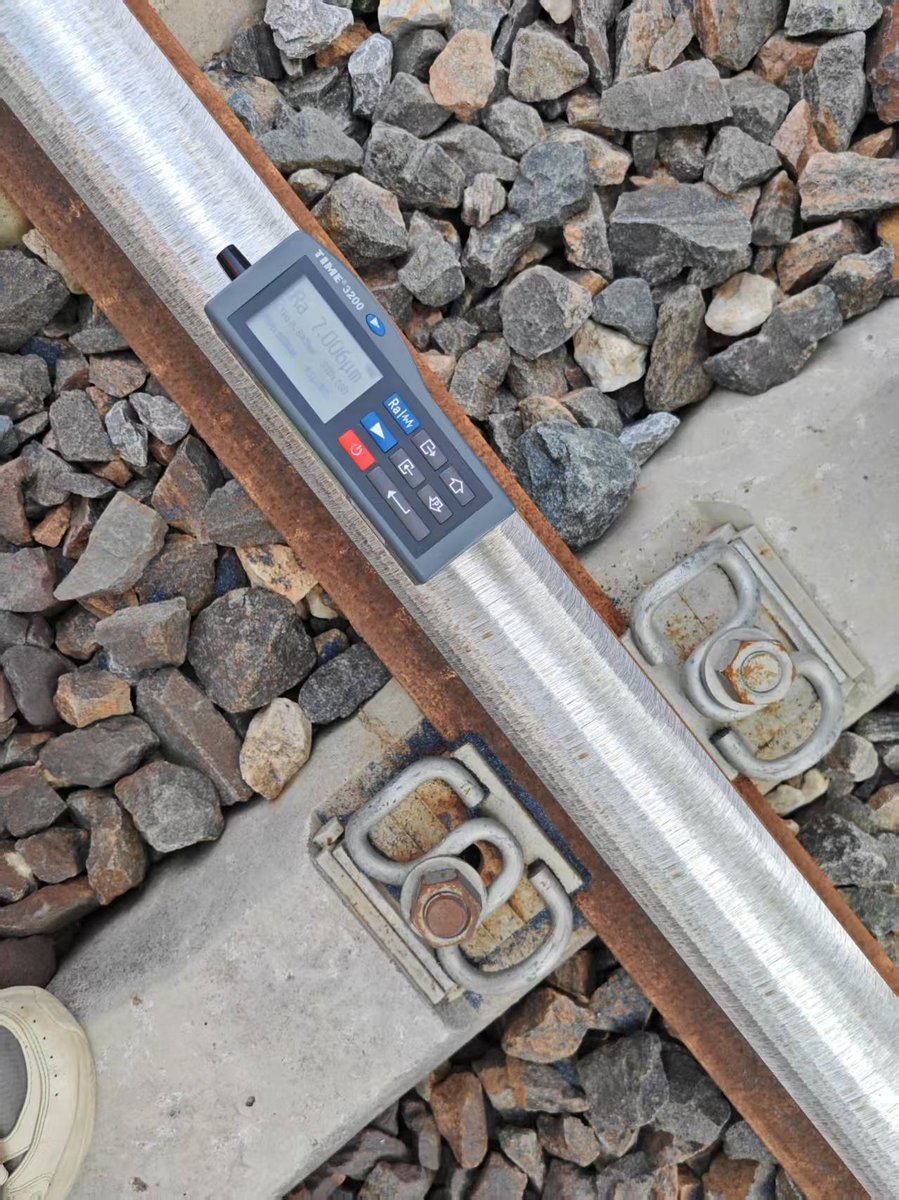
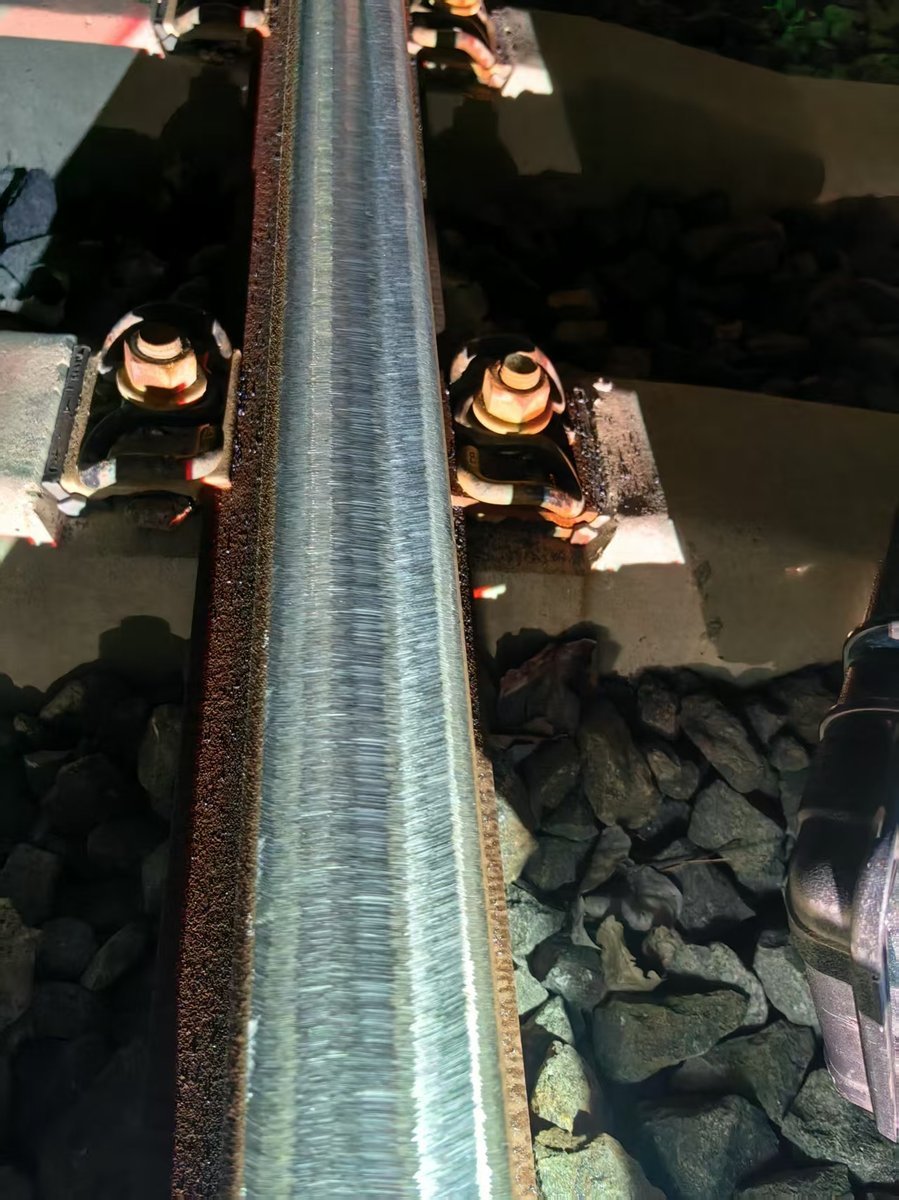
Contact RailwayCare today to learn how our expert rail grinding services can enhance the performance and safety of your railway infrastructure. Let us help you keep your trains running smoothly and safely.
• Website Product list page: www.railwaycare.com
• Email: simon.wang@railwaycare.com
• WhatsApp: +86 15072332788
Your tracks are our priority. Choose RailwayCare for reliable rail maintenance and superior rail grinding expertise.
FAQ
What causes rail burn during grinding?
Five causes account for most incidents: a bond too hard to shed dull grain, grinding pressure too high, speed too low so contact time per unit length rises, insufficient porosity so heat cannot be carried away, and poor chip clearance so swarf is re-ground. Four of the five are decided when the wheel is specified, which is why wheel selection is the most effective control. The parameters that interact here are quantified in high-speed grinding operating parameters.
How do you detect a rail burn after grinding?
Visual inspection for blue-black discolouration is the first screen, but it cannot find sub-surface damage — magnetic particle testing reveals the thermal cracks, portable hardness testing flags martensite above roughly 450 HV, and nital etching is the definitive check for a white etching layer. All four methods and the acceptance limits they support are set out in rail grinding acceptance standards.
Can a rail burn be ground out?
It can, but only by removing the entire affected layer — typically 0.3–0.5 mm of rail material — and the metallurgical change is permanent until that is done, because martensite cannot be tempered back in track. The practical alternative is prevention, since a burn severe enough to require re-grinding costs far more than the wheel that would have avoided it.
Which railway grinder wheel specification prevents burning?
Self-sharpening grain (zirconia alumina), a controlled hot-pressed bond, engineered porosity above about 15%, finer grain in the 24–36 grit range, and uniform density to avoid hot spots. Wheel specification is also the difference between domestic and imported supplies at equal performance — the comparison method is in domestic vs import railway grinder wheels, and the matching of formulation to machine in wheel selection by grinding vehicle.
What grinding speed avoids rail burn?
Burn risk rises sharply as speed falls below about 4 km/h, because contact time per unit area increases and heat accumulates faster than the rail can dissipate it. In our own heavy-haul work with a Harsco 96 the campaign ran at 6–10 km/h for 200+ km with zero burn incidents and an average of 6.2 µm Ra, which is the window we would recommend as a starting point.
Eliminate Rail Burns From Your Operation
Contact Molaton for a burn-prevention consultation. We will analyze your current grinding parameters and recommend a zero-burn railway grinder wheel solution.
Request Burn Prevention Consultation →