What railroad maintenance machines are used for inspection?
What railroad maintenance machines are used for inspection?
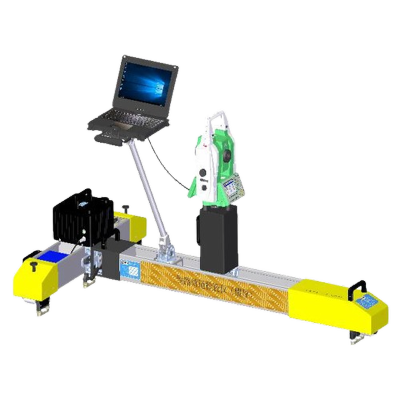
Four families do the work: track geometry inspection trolleys and recording cars (gauge, cross level, twist, alignment, longitudinal level, versine), rail defect detection, image-based structure inspection of rail, fastenings, sleepers and ballast, and the hand verification kit — running band, roughness and a 1 m straightedge — that closes the grinding loop.
The four inspection families and the numbers they report
| Family | What it inspects | Figures to expect |
|---|---|---|
| Track geometry trolley / recording car | Gauge, gauge variation rate, cross level and superelevation, twist (two-level difference), alignment and longitudinal level, versine, distance | Gauge and cross level to about ±0.3 mm, twist ±0.5 mm on a 2.4 m base, alignment and level ±0.7 mm on 10 m and 30 m chords, versine ±1.0 mm, long-chord level ±3.0 mm on 300 m, odometer ±0.1% |
| Rail defect detection | Internal flaws and surface damage that justify a grinding or replacement decision | Defect location and severity, logged against distance so it can be re-found in the next possession |
| Image-based structure inspection | Rail surface, fastenings, sleepers, ballast and transitions, with automatic defect judgement | Cameras around 1280×720 at 60 fps global shutter, recording roughly 6 GB per hour, about 18 hours of day use or 6 hours at night on one battery set |
| Hand verification kit | The finished surface: running band width, roughness, flatness, burning | Running band 25–30 mm on high-speed turnouts and 35–40 mm on conventional and heavy-haul turnouts; Ra ≤ 10 μm; flatness within 0.3 mm under a 1 m straightedge |
Working speed matters as much as accuracy. Inertial-plus-total-station trolleys verify at roughly 1.5–3 km/h, while relative-measurement trolleys and self-propelled units run at 4–6 km/h or better — which is what makes a full section check possible inside a short possession.
Why inspection only pays off as a closed loop
Measured data has to feed the work order, or it is just a report. The productive sequence is: pre-measure with the inspection trolley, generate the work files and import them into the machine's computer, let the adjustment software optimise the plan, work to that plan, re-measure, then export the alignment, level, gauge, cross level and TQI reports for line quality evaluation. On the Taiyuan network, precision tamping delivered to a measured plan across nine sections totalling 15.28 km took average static TQI from 7.19 to 4.52 and average dynamic TQI from 7.64 to 4.67 — an improvement you can only claim because it was measured twice.
For grinding, the grading language is the same idea. A grinding quality index of GQI ≥ 85 is graded excellent and ≥ 70 acceptable, with a standard deviation limit across the section so a good average cannot hide a bad 200 m. A poor result is also measurable: running the machine at the wrong speed and depth leaves a brittle white layer of about 870 HV0.3 against roughly 340 HV0.3 for the parent metal, while in the same test series surface roughness moved from 6.6 to 8.4 μm as grinding speed rose from 1,000 to 3,000 rpm. None of that would be visible without instruments.
Case and data — what measurement catches
On the Liuzhou network a GMC-96X running Molaton wheels ground 18.72 pass-kilometres in one two-hour possession, with CYF wheels consuming 20–30 mm against 43.5–59 mm for the imported wheels — a difference only the consumable records could prove. On Hewu high-speed line the verified comparison was 4.28 versus 3.27 pass-kilometres per millimetre, with a best wheel of 214.22 pass-kilometres and no continuous blue burning; independent testing at the China Academy of Railway Sciences measured wear 1.4–2.6× better than specification. On the Loram DM01 machine tested in 2026, inspection of the finished surface returned no blue burning and roughness of Ra 1.05–9.0 μm, mostly 2–4 μm.
Inspection also captures the benefit that operators care about most. Where turnout profiles were corrected and verified, car-body lateral acceleration fell from about 0.20 m/s² to 0.04–0.08 m/s². That measurement is the argument for the next budget, and it is the reason RailwayCare has supplied rail grinding wheels since 2004 — the first dedicated producer in China — to the standard JB/T 11431 the company drafted.
Related questions you may also ask
How does a grinding train remove rail defects? What is track maintenance and what does it include? Rail head grinding: restoring the contact surfaceClose the loop between measurement and grinding
Send us the geometry report, the machine you run and the profile you need to hold. We will come back with the wheel specification, the expected surface finish and the acceptance numbers to verify on site.
Request a Verification PlanInspection and measurement tooling sits alongside the rest of the range in railway inspection tools, and the whole programme is set out in the rail maintenance solution.
Are you looking for a reliable manufacturer of railway grinding and track maintenance equipment?
We can quickly provide customers with market analysis, technical support and customized services.
Safe Tracks Proven by China
- Name
- Phone
- *Title
- *Content