What railway track maintenance equipment is essential?
What railway track maintenance equipment is essential?
Seven items are essential: a verified way to measure track geometry, a grinding capability, rail cutting and drilling, tamping and lift-and-line, fastening and bolt tools, traceable consumable records, and a possession plan that fits the work into the access you actually get. Everything else is an optimisation of those seven.
The essential seven, and what each one has to deliver
| Essential | Why it is essential | Specification to insist on |
|---|---|---|
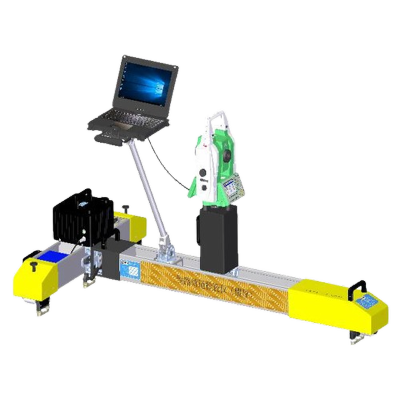
| 1. Geometry measurement | You cannot judge a grinding pass, a tamping shift or a renewal against memory — only against a before-and-after baseline | Gauge, cross level, twist, alignment, longitudinal level and versine, reported per section so a trend is visible |
| 2. Grinding | The only way to remove corrugation and the fatigued layer without cutting the rail out of the track | 16 grit zirconia alumina in a glass-fibre reinforced resin bond, dimensioned to the machine seat, rated at least 50 m/s |
| 3. Rail cutting and drilling | Joint replacement, closures and insulated joints stop the whole programme if they need a contractor call-out | Cutting discs 356×4×25.4, 400×4×32, 305×3.6×22.2 or 180×3×22.2, brown fused alumina, 80–100 m/s |
| 4. Tamping, lifting and lining | Grinding removes metal and ballast work disturbs geometry; the profile is only useful if the geometry is restored around it | A work plan the machine can actually import, and a pass that finishes inside the geometry tolerance |
| 5. Fastening and bolt tools | The assembly holds the profile you just ground; loose or over-torqued fastenings undo the work | Correct torque capability and battery commonality with the rest of the tool fleet |
| 6. Consumable records | Pass-kilometres per millimetre of wheel consumed is the only number that makes the next tender comparable | Batch traceability: dynamic balance, storage condition and rejection rules for wheels dropped or stored wet |
| 7. Possession plan | On a live railway the window, not the machine, is the binding constraint |
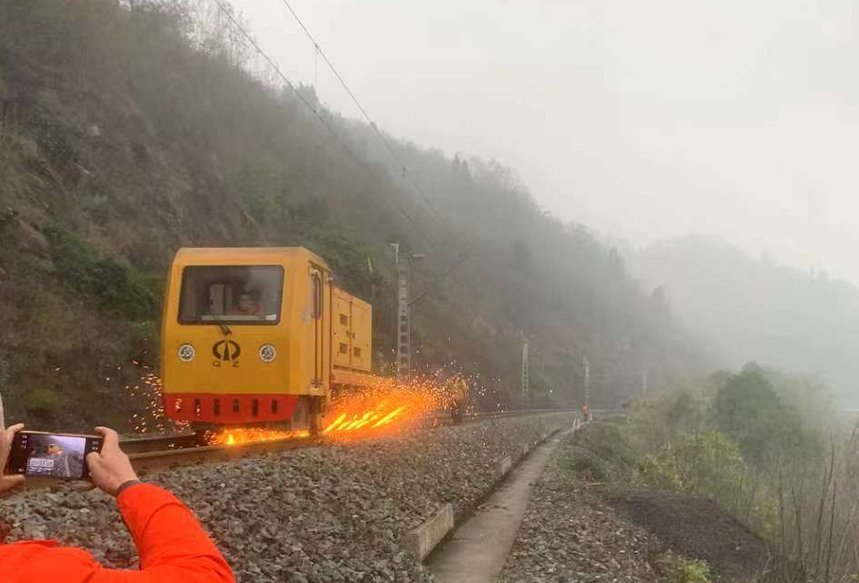
The consumable is part of the equipment, so specify it like equipment
| Machine | Wheel size (mm) | Bond and abrasive | Grit | Maximum speed |
|---|---|---|---|---|
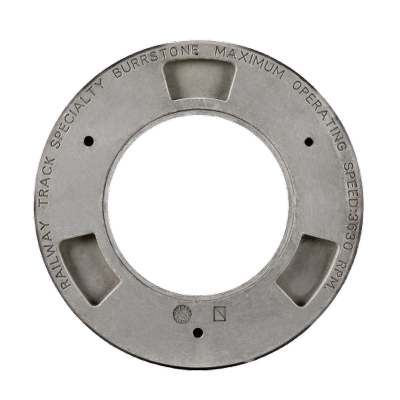
| Harsco PGM-48 / PGM-96C grinding trains | 260×90×154 | Aluminium matrix + zirconia alumina + glass fibre, ZA/F16 Y5B | 16 | 50 m/s, 3,630 rpm |
| Harsco RGH20C turnout grinder | 280×25.5×116 | Iron matrix + zirconia alumina + glass fibre | 16 | 50 m/s, 3,630 rpm |
| GMC16A grinding train | 350×60 / 25 / 50 / 35×127 | Resin bond, zirconia alumina | 16 | 2,730 rpm |
| GMC96B grinding train | 180×105×90 | Resin bond, zirconia alumina | 16 | 6,000 rpm |
| Loram grinding trains | 260×83×154 and 250×75×150 (G3) | Aluminium matrix + zirconia alumina + glass fibre | 16 | 3,630 / 3,280 rpm |
| Mecno grinding trains | 350×25×127 | Resin bond, zirconia alumina | 16 | 50 m/s |
| Portable machines (Geismar, Robel, and similar) | 150×56×M20, 150×70×M20 | ZA/F16 Y5B | 16 | 6,000–7,500 rpm |
| Rail cutting machines | 356×4×25.4, 400×4×32, 180×3×22.2 | Brown fused alumina ZA/F30 | 30 | 80–100 m/s |
A wheel that is dimensionally wrong, under-rated for speed or out of balance is not a cheaper wheel — it is a safety and rework problem. That is why the essential list includes records, not just hardware. The railway grinding wheel range is dimensioned machine by machine for exactly this reason.
Case and data — what the essential kit returns
On the Liuzhou network a GMC-96X running Molaton wheels ground 18.72 pass-kilometres in one two-hour possession. On Hewu high-speed line the measured comparison was 4.28 against 3.27 pass-kilometres per millimetre, with a best wheel of 214.22 pass-kilometres and no continuous blue burning. On the Yiyang railway a wheel reached 5.7 pass-kilometres per millimetre, on Shuohuang 4.98, and a 600-wheel batch passed Shenhua acceptance. Independent testing at the China Academy of Railway Sciences recorded wear 1.4–2.6× better than specification.
Just as important is what grinding at the right speed and depth avoids. A badly run pass leaves a brittle white layer of about 870 HV0.3 against roughly 340 HV0.3 for the parent metal — about 155% harder. That layer fractures early, sends fragments into the parent metal and initiates cracks from there, which is why depth is held to 0.2–0.3 mm per pass. On the Loram DM01 machine tested in 2026 the wheels produced no blue burning and surface roughness of Ra 1.05–9.0 μm, mostly 2–4 μm. Where turnout profiles were corrected, car-body lateral acceleration fell from about 0.20 m/s² to 0.04–0.08 m/s².
RailwayCare has built wheels behind these results since 2004 — the first dedicated rail grinding wheel producer in China — and drafted the industry standard JB/T 11431. The full programme, from wheels to machines, is set out in the rail maintenance solution.
Related questions you may also ask
What is track maintenance and what does it include? What is a rail grinder train and how does it work? Rail grinding cost per kilometre: what operators payTurn the essential list into a working kit
Tell us your line types, annual tonnage, the machines you already own and the windows you can get. We will confirm the essential gap, the wheel specification for each machine and the pass-kilometres per millimetre to expect.
Request a Kit ReviewGrinding is only one of the seven essentials — the wider tool set is listed in railway maintenance tools.
Are you looking for a reliable manufacturer of railway grinding and track maintenance equipment?
We can quickly provide customers with market analysis, technical support and customized services.
Safe Tracks Proven by China
- Name
- Phone
- *Title
- *Content